Welding Wire
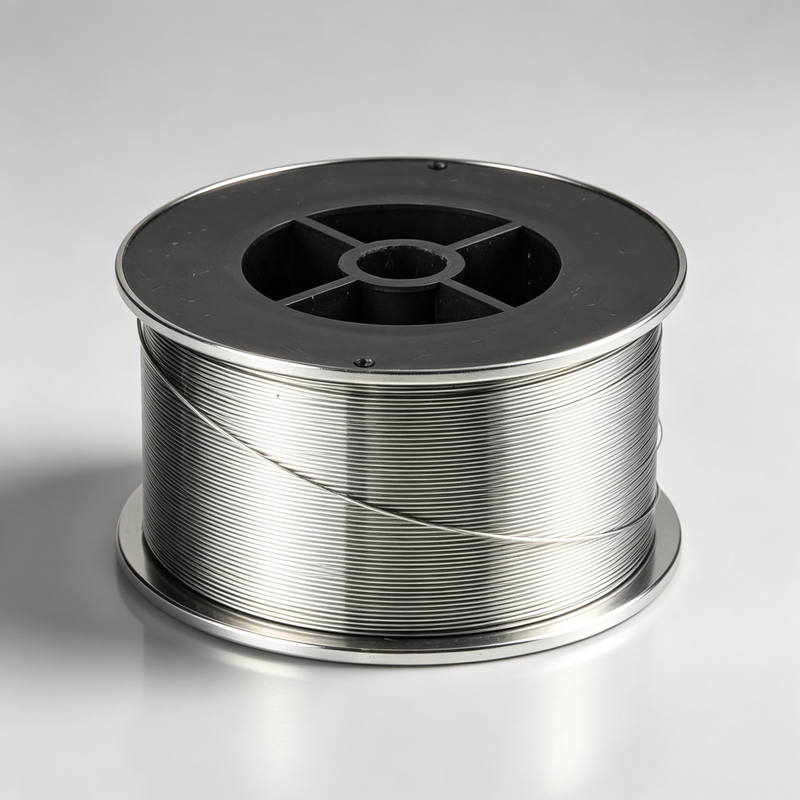
Solid and flux-cored welding wires for MIG/MAG, arc spray, PTA and laser cladding.
We provide solid and flux-cored welding wires for construction machinery, petrochemical, power, mining and metallurgy industries, supporting dimensional restoration and surface strengthening.
Solid wires feature uniform composition, low spatter and smooth weld formation, compatible with MIG/MAG surfacing, arc spraying and laser cladding. SS420 stainless steel wire delivers moderate hardness and wear & corrosion resistance for hydraulic props, valve seals and molds. Ni20Al nickel-aluminum wire offers high bonding strength and high-temperature oxidation resistance, serving as thermal spray bond coat or boiler tube protection.
Flux-cored wires enable flexible alloy adjustment via core formulation, with high deposition efficiency for heavy-load wear and high-temperature corrosion scenarios. The representative FeCrBSi self-fluxing wire boasts high hardness and excellent abrasive wear resistance, widely used for wear repair of rolls, crusher hammers and conveyor components.
Key Attributes
- Diameter 1.2mm, 1.6mm, 2.0mm, 2.4mm, 3.2mm
- Grade Series NE-W
- Brand NE Tool
Welding Wire - Grade Selection
31 grades available in this series. Custom particle-size cuts and chemistries available on request.
| Product Grade | Chemical Composition | Manufacturing Process | Hardness (HRC) | Application Process | Typical Application |
|---|---|---|---|---|---|
| NE-W-Fe420 | Mn:0.5, C:0.32, Ni:0.5, Cr:13.0, Si:0.25, Fe:Bal | DR | 55-60 | PTA/LC/AS | Excellent corrosion and wear resistance; harder, thicker coating with low shrinkage and good wear resistance |
| NE-W-Fe316L | Mn:1.5, C:0.03, Ni:12.5, Cr:18.5, Mo:2.4, Si:0.45, S:0.005, P:0.02, Cu:0.2, Fe:Bal | DR | 22-28 | AS/FS/PTA/LC | Anti-corrosion for chemical & seawater equipment, pressure vessel welding, hydraulic part restoration |
| NE-W-Fe95 | C:<0.1, Si:1.5-2, Mn:1.5-2, Cr:27-29, B:3.5-4.0, Fe:Bal | DR | 55-60 | FS/PTA/LC/AS | Flame spray welding for valves, rollers, slurry pumps and mining parts |
| NE-W-FeE97 | WC:26.2, Si:1.3, Cr:13.8, TiC:6.2, Ni:5.5, B:1.92, Mn:0.58 | DR | 60-65 | PTA/AS/LC/FS | Impact-resistant coating for crushers, bucket teeth, conveyor rollers |
| NE-W-Fe410 | Mn:0.5, C:0.11, Ni:0.14, Cr:13.0, Si:0.31, S:0.002, P:0.021, Fe:Bal | DR | 36-42 | PTA/LC/AS | Cavitation-resistant surfacing for pumps & turbine blades, martensitic steel welding |
| NE-W-Fe304 | Mn:1.5, C:0.08, Ni:9.5, Cr:19.0, Si:0.50, S:0.02, P:0.01, Fe:Bal | DR | 20-26 | AS/FS/PTA/LC | General stainless steel welding, anti-corrosion coating for papermaking machinery |
| NE-W-Fe55 | C:4.5-5.5, Si:0.7-1.5, Mn:0.7-1.5, Cr:27-29, Fe:Bal | DR | 55 | FS/PTA/LC/AS | High-hardness surfacing for plungers, sleeves, construction & metallurgical rollers |
| NE-W-FeLC | Mn0.8; Si0.2; C0.15; FeBal | VIM | 95-100 HRB | AS/FS | Bearing, seating surfaces, economical option |
| NE-W-FeHC | 0.8C, 0.7Mn, 0.3Si, BalFe | VIM | 20-25 | AS/FS/LC | Low shrink, shafts, housing, pistons, fans |
| NE-W-FeCrAl | Bal Fe, 23.5Cr, 5.3Al, 0.45Mn, 1Si | VIM | 85-90 HRB | AS/FS/LC | Boiler tubes, dimensional restoration |
| NE-W-Fe26CrNi | 26Cr, 3Ni, 1.7C, 1.6Mn, 1.6Si, 0.8Mo, Bal Fe | VIM | 39-42 | AS/PTA/LC/FS | Good corrosion & wear, machineable |
| NE-W-Fe29CrB | 29Cr, 3.7B, 1.7Mn, 1.5Si, Bal Fe | VIM | 55-60 | AS/PTA/LC/FS | Abrasion resistance, rolls, boiler tubes |
| NE-W-Ni20Al | 20Al, Bal Ni | VIM | 75 HRB | AS/FS/PTA/LC | Bond coats |
| NE-W-Ni5Al | 93Ni, 4.0-5.5Al, 1.7max Other | VIM | 75 HRB | AS/FS/PTA/LC | Bond coats, turbine engine part buildup |
| NE-W-NiCrAl | 20Cr, 7Al, Bal Ni | VIM | 85-95 HRB | AS/FS/PTA/LC | Oxidation resistance, ceramic undercoat |
| NE-W-NiCrAlY | Bal Ni, 22Cr, 10Al, 1Y | VIM | 60-85 HRB | AS/FS/PTA/LC | Oxidation resistance, ceramic undercoat |
| NE-W-Ni718 | Ni bal, Cr<20%, Fe<20%, Mo<5%, Ti<5%, AlCoNiMnSi<1% | VIM/VAR | 30 | AS/FS/PTA/LC | Oxidation resistance, turbine engines |
| NE-W-Ni625 | 62.5Ni, 22Cr, 10Mo, 2Fe, 3.5Cb+Ta | VIM | 92 HRB | AS/FS/PTA/LC | Oxidation resistance, corrosion resistance, digesters |
| NE-W-NiC276 | C<=0.02, Cr:14.5-16.5, Mo:15.0-17.0, W:3.0-4.5, Si<=0.08, Fe:4.0-7.0, Mn<=1.0, Co<=2.5, P<=0.04, S<=0.03, V<=0.35, Cu<=0.5, Ni:Bal | VIM+ESR/VDR | 18-24 | AS/FS/PTA/LC | Surfacing for FGD system, chemical anti-corrosion equipment, pickling facilities |
| NE-W-NiCu | Ni>=63, Cu:28-34, Fe<=2.5, C<=0.3, S<=0.015, P<=0.015, Mn<=2.00, Si<=0.5 | VDR | 15-22 | AS/FS/PTA/LC | Seawater equipment, hydrofluoric acid service, marine pumps & valves, cavitation-resistant coating |
| NE-W-Ni20Cr | C<=0.10; Si0.75-1.60; Mn<=0.6; Cr20.0-23.0; Al<=0.50; Mg<=0.10; S<=0.005; P<=0.002; Fe<=1.0; Cu<=0.10; Others<=0.5; Ni Bal | VDR | 20-35 | AS/FS/PTA/LC | High-temperature oxidation resistant coatings, furnace parts, boiler tubes, paper mill rolls |
| NE-W-Co01 | Cr25.5; W12.5; C1.9; Others<5; Co Bal | VIM | 48-54 | PAW/GTAW/GMAW/PTA/LC/AS | Hydropulper disc, mixer blades & rotors, conveyor screws, pump sleeves |
| NE-W-Co06 | Cr20-35; W0.1-10; Fe0.1-5; C0.1-5; Si0.1-5; Mn0.1-5; Co Bal | VIM | 40-44 | PAW/GTAW/GMAW/PTA/LC/AS | Valve seats, bearing areas, extrusion screw flights and tong bits |
| NE-W-Co12 | Cr20-35; W5-10; Fe0.1-5; C0.1-5; Si0.1-5; Mn0.1-5; Co Bal | VIM | 43-49 | PAW/GTAW/GMAW/PTA/LC/AS | Chain saw bars, hot extrusion dies, tong bits, exhaust valves and metal-to-metal sliding |
| NE-W-Co21 | Cr25.0-30.0; Ni1.50-4.0; Mo4.50-7.0; C0.15-0.45; Mn<=1.50; Si<=1.50; W<=0.50; Fe<=3.00; Others<=0.50; Co Bal | VIM | 33-37 | PAW/GTAW/GMAW/PTA/LC/AS | Great resistance to corrosion, galling, cavitation and metal-to-metal wear for valves |
| NE-W-Mo | Mo 99.9; Others<=0.01 | VIM | 10-20 | PAW/GTAW/GMAW/PTA/LC/AS | Molybdenum wire for metal thermal spraying |
| NE-W-CuAl | Al7.5-9.5; Fe<0.5; Mn<1.0; Ni<0.8; Pb<0.02; Si<0.2; Zn<0.2; Cu Bal | DR | 20-35 | AS/FS/PTA/LC | Excellent fluidity, uniform weld beads; steel-copper dissimilar welding |
| NE-W-Cu | Cu 99.95; Others<=0.05 | DR | 15-30 | AS/FS/PTA/LC | Electrical and thermal conductive coatings, corrosion-resistant coatings for marine environments |
| NE-W-CuNiAl | Al7.5-9.5; Fe3.0-5.0; Mn0.6-3.5; Ni4.0-5.5; Pb<=0.02; Si<=1.0; Zn<0.10; Others<=0.5; Cu Bal | DR | 20-35 | AS/FS/PTA/LC | Marine pump & valve repair, corrosion & cavitation resistant coatings, steel-copper dissimilar welding |
| NE-W-CuAlFe | Al8.0-10.0; Fe2.0-4.0; Mn<0.5; Ni<0.5; Pb<0.02; Si<0.1; Zn<0.1; P<0.01; Sn<0.1; Cu Bal | DR | 20-35 | AS/FS/PTA/LC | Bearing & bushing repair, corrosion resistant coatings for marine & chemical equipment |
| NE-W-ZnCuNi | Cu46.0-50.0; Ni9.0-11.0; Al<=0.01; P<=0.25; Pb<=0.05; Si0.04-0.25; Others<=0.5; Zn Bal | DR | 20-35 | AS/FS/PTA/LC | Long-term cathodic protection for steel structures, bridges, ships, towers and pipelines |
How to Specify & Apply
Identify the Service Envelope
Determine the dominant wear mode (abrasion, erosion, adhesion, corrosion, oxidation), operating temperature and impact load. This narrows the grade selection to 2-3 candidates.
Match the Process
Each grade is validated for specific deposition processes. The "Application Process" field above shows HVOF, HVAF, APS, PTA, LMD, OFS or CAW compatibility.
Choose the Particle Size
Particle size controls deposit density and surface finish. Fine cuts (15-30um) for thin dense coatings; coarser cuts (45-90um) for thick build-up and high deposition rate.
Request a Sample
Most grades ship with a 1-2 kg sample for in-house process qualification. Our engineers will support parameter development on your equipment.
Other Products in Welding Materials
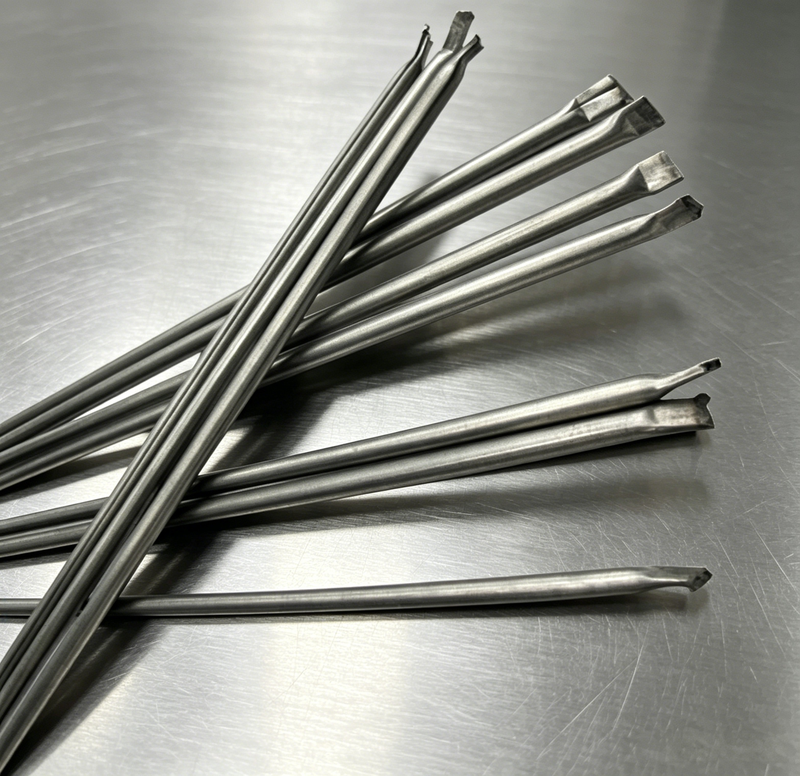
Tungsten Carbide Tube Welding Rod
Mild-steel-sheath tube rods filled with WC for oxy-acetylene hardfacing.
View →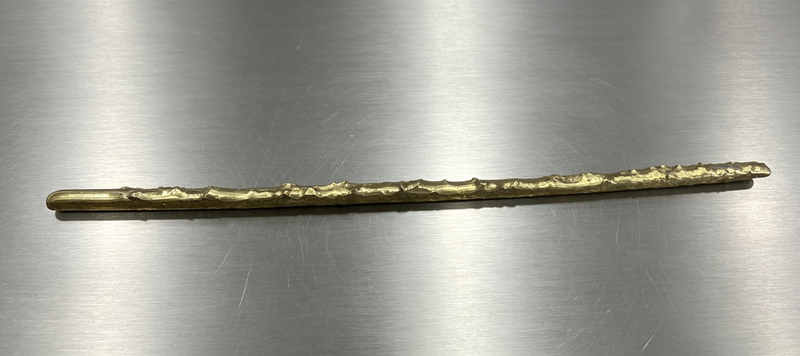
Tungsten Carbide Composite Welding Rod
WC-Co hard particles in copper-based bonding alloy for oil & gas downhole tool hardfacing.
View →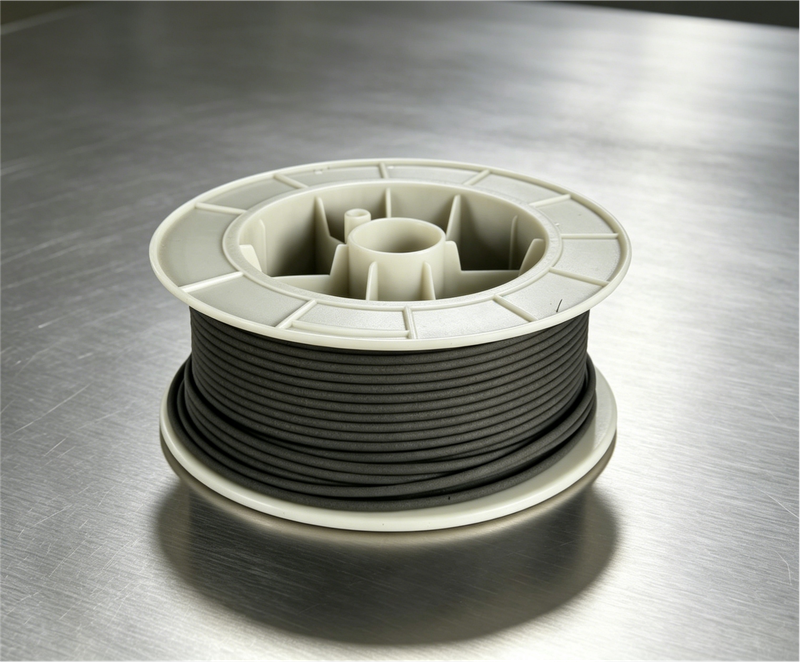
Tungsten Carbide Flexible Welding Rope
Flexible braided wire with cast WC and Ni-based self-fluxing alloy for irregular part repair.
View →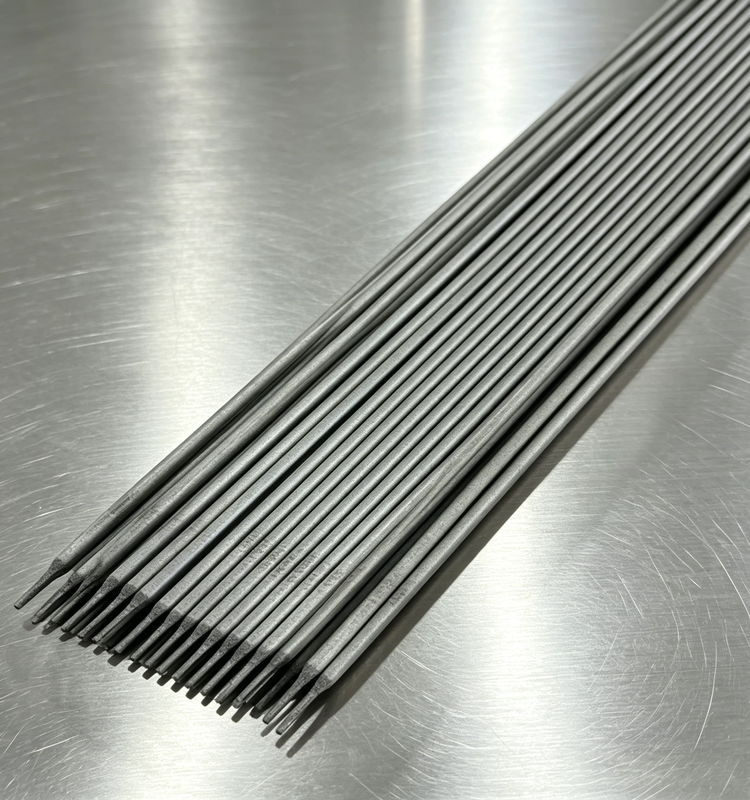
Cobalt-Based Welding Rod
Stellite-equivalent Co-Cr-W bare cast rods and coated electrodes for manual & automated hardfacing.
View →