Nickel-Based Alloy Powder
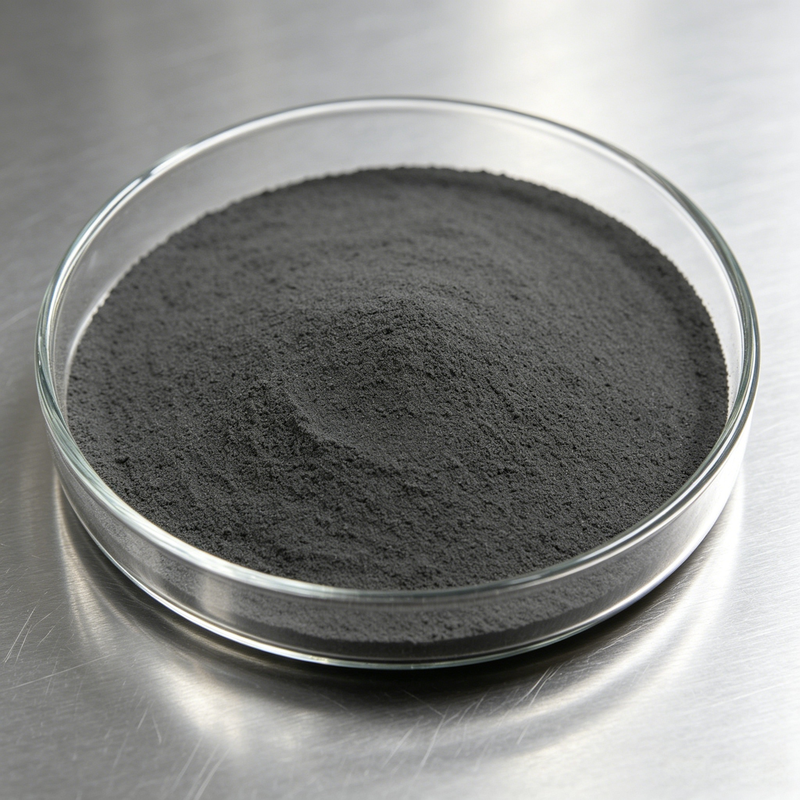
Ni-Cr-B-Si self-fluxing alloy powders for spray-and-fuse, PTA and laser cladding.
Nickel-based alloy powders are a type of high-performance powder materials produced with nickel as the matrix and added with alloying elements such as chromium, molybdenum, tungsten, boron, silicon and carbon.
With high cost-effectiveness, excellent corrosion resistance and good process compatibility, they have become one of the most widely used consumables for surface strengthening processes including thermal spraying, plasma surfacing and laser cladding.
These powders are fully compatible with the operational requirements of high-velocity oxygen-fuel spraying equipment (HVOF), plasma surfacing equipment and laser cladding equipment, and can balance the improvement of component surface performance and the control of production costs.
Key Attributes
- Manufacture Process Gas Atomized
- Particle Size 15-45um, 20-53um, 45-90um, 20-106um, 45-106um, 45-125um, 53-125um, 53-150um
- Grade Series NE-Ni
- Brand NE Tool
- Application Process HVOF, APS, Laser Cladding, PTA Welding
Nickel-Based Alloy Powder - Grade Selection
15 grades available in this series. Custom particle-size cuts and chemistries available on request.
| Product Grade | Chemical Composition | Apparent Density (g/cm3) | Hardness (HRC) | Manufacturing Process | Application Process | Typical Application |
|---|---|---|---|---|---|---|
| NE-Ni-015A | C0.03, Cr0.46, Si2.3, Fe<=0.50, Mn0.09, B0.9, Cu0.2, Ni:Bal | 4.60-4.70 | 15 | Gas Atomization | HVOF/APS/LMD | Bond coat for WC series spray welding coatings |
| NE-Ni-020 | C:0.03, Cr:4.50, Si:2.00, B:0.70, Ni:Bal | 4.58-4.68 | 20 | Gas Atomization | HVOF/APS/LMD/OFS | Glass molds and various forming molds |
| NE-Ni-022A | C:0.20, Cr:0.10, Si:2.85, Fe<=0.50, Mn:0.50, B:1.45, Ni:Bal | 4.57-4.67 | 22 | Gas Atomization | OFS/PTA/HVOF/LMD | Glass molds and various forming molds |
| NE-Ni-020PTA | C:0.05, Cr:1.00, Fe<=0.15, B:0.90, Ni:Bal | 4.59-4.69 | 20 | Gas Atomization | OFS/PTA/HVOF/LMD | Precision glass mold repair & surfacing |
| NE-Ni-022PTA | C:<=0.05, Cr:4.50, Si:3.80, Fe<=3.00, Mn:0.30, B:1.00, Ni:Bal | 4.58-4.68 | 28 | Gas Atomization | PTA/HVOF/HVAF/LMD | Precision glass mold repair & surfacing |
| NE-Ni-030A | Ni Bal, 7Cr, 4Si, 1.1B | 4.54-4.64 | 30 | Gas Atomization | OFS/PTA/HVOF/LMD | Pulleys, gear tooth surface repair |
| NE-Ni-035 | Ni Bal, Cr4, Si3, Fe1.4, B1.5 | 4.52-4.62 | 35 | Gas Atomization | OFS/PTA/HVOF/LMD | Shaft parts, molds, valve and pump components, power machinery and chemical equipment |
| NE-Ni-035AA | C:0.20, Cr:8.00, Si:3.20, Fe<=3.00, Mo:0.10, Mn:0.10, B:1.60, Ni:Bal | 4.53-4.63 | 35 | Gas Atomization | OFS/PTA/HVOF/LMD | Glass molds, valve seats |
| NE-Ni-040A | Ni Bal, 7.5Cr, 1.7B, 3.5Si | 4.50-4.60 | 40 | Gas Atomization | OFS/PTA/HVOF/LMD | Heavy-load wear-resistant, corrosion-resistant and high-temperature oxidation-resistant parts, covering shafts, valves, molds, mining/petroleum tools, power machinery and chemical equipment |
| NE-Ni-045A | C:0.05, Cr:8.00, Si:3.50, Fe<=10.00, B:2.00, Ni:Bal | 4.49-4.59 | 45 | Gas Atomization | OFS/PTA/HVOF/LMD | Screw feeder, mold core |
| NE-Ni-050 | Ni Bal, 16Cr, 4B, 4Si, 3Fe | 4.46-4.56 | 50 | Gas Atomization | OFS/PTA/HVOF/LMD | Extrusion screws, fan blades, extruder barrel liners, valve seats, pump sleeves |
| NE-Ni-055 | Ni Bal, 16Cr, 4B, 4Si, 3Fe | 4.45-4.55 | 55 | Gas Atomization | OFS/PTA/HVOF/LMD | Heavy wear parts: screw conveyors, fan blades, extruder barrels, plungers, sleeves |
| NE-Ni-060 | Ni Bal, 16Cr, 4B, 4Si, 3Fe | 4.44-4.54 | 60 | Gas Atomization | OFS/PTA/HVOF/LMD | High-hardness wear components: extrusion screws, sleeve, mold edges, plunger repair |
| NE-Ni-060AA | C:0.8, Cr:16, Si:4.5, B:3.5, Fe:3, Mo:3, Cu:3, Ni:Bal | 4.43-4.53 | 60 | Gas Atomization | OFS/PTA/HVOF/LMD | High-wear parts: crusher segments, fan blades, screw conveyors, sleeves |
| NE-Ni-065 | C:1.0, Cr:18, Si:4.5, B:3.5, Mo:2, Cu:2, Ni:Bal | 4.42-4.52 | 65 | Gas Atomization | OFS/PTA/HVOF/LMD | High-impact wear parts: crusher hammers, fan blades, sleeve guides |
How to Specify & Apply
Identify the Service Envelope
Determine the dominant wear mode (abrasion, erosion, adhesion, corrosion, oxidation), operating temperature and impact load. This narrows the grade selection to 2-3 candidates.
Match the Process
Each grade is validated for specific deposition processes. The "Application Process" field above shows HVOF, HVAF, APS, PTA, LMD, OFS or CAW compatibility.
Choose the Particle Size
Particle size controls deposit density and surface finish. Fine cuts (15-30um) for thin dense coatings; coarser cuts (45-90um) for thick build-up and high deposition rate.
Request a Sample
Most grades ship with a 1-2 kg sample for in-house process qualification. Our engineers will support parameter development on your equipment.
Other Products in Alloy Powder
Cobalt-Based Alloy Powder
Co-Cr-W Stellite-equivalent powders for extreme wear and high-temperature service.
View →
Ferro-Based Alloy Powder
Cost-effective Fe-Cr-B-C self-fluxing alloy powders for general wear and repair.
View →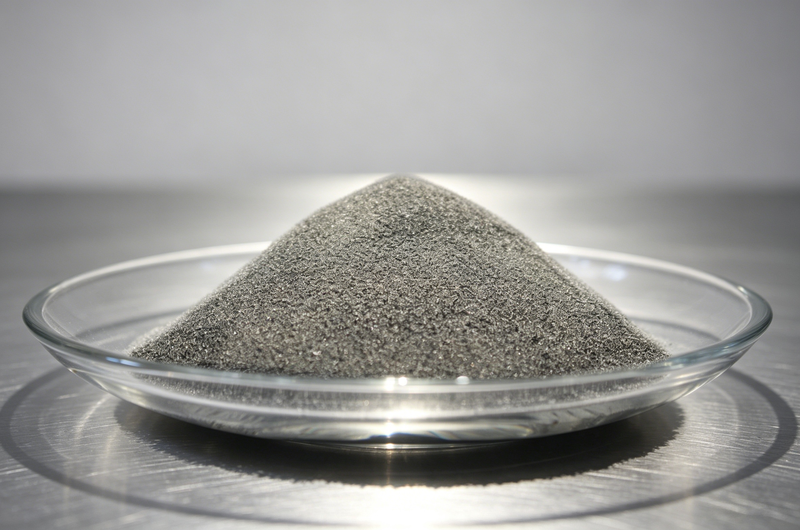
Nickel Powder Mixed with Cast Tungsten Carbide (PTA)
Ni60-based PTA hardfacing powder loaded with cast tungsten carbide for extreme abrasion.
View →