Ferro-Based Alloy Powder
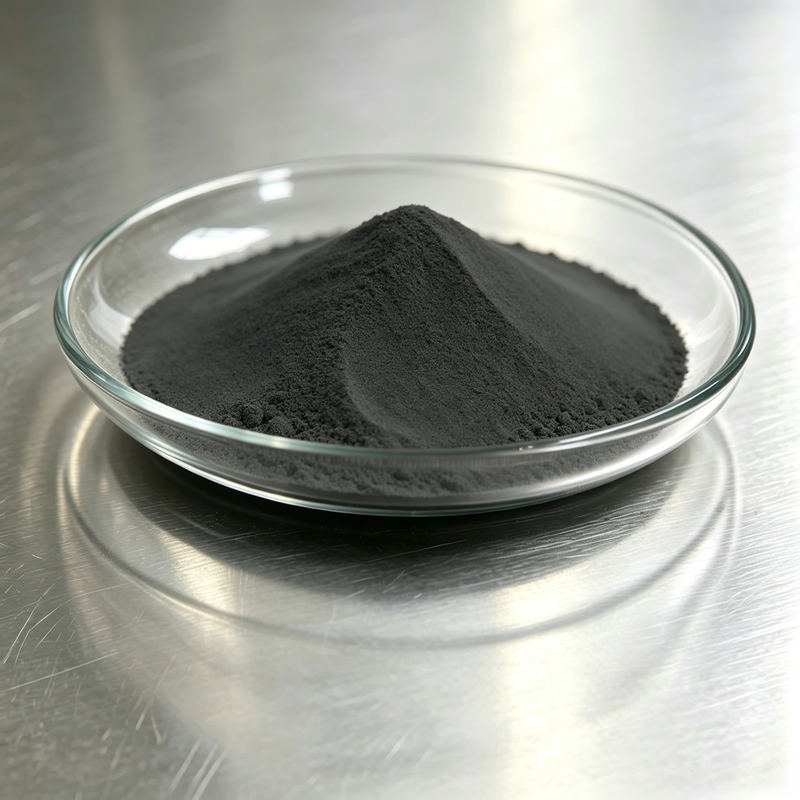
Cost-effective Fe-Cr-B-C self-fluxing alloy powders for general wear and repair.
Ferro-based alloy powders use iron as the matrix, alloyed with chromium, carbon, boron and silicon. They offer high hardness, good abrasive wear resistance and a cost-effective alternative to nickel- and cobalt-based materials for less severe-duty applications.
Their self-fluxing properties enable them to be applied by oxy-acetylene flame spray-and-fuse, PTA welding, plasma spray and laser cladding, producing dense, metallurgically bonded overlays for wear repair of rolls, plows, screw conveyors and mining components.
For applications where cost-per-kilo of deposited material is a key factor - such as agricultural machinery, construction equipment and steel mill rolls - ferro-based powders provide the optimal balance of performance and economy.
Key Attributes
- Manufacture Process Gas Atomized / Water Atomized
- Particle Size 15-45um, 20-53um, 45-90um, 53-125um
- Grade Series NE-Fe
- Brand NE Tool
- Application Process HVOF, APS, Laser Cladding, PTA Welding, OFS
Ferro-Based Alloy Powder - Grade Selection
8 grades available in this series. Custom particle-size cuts and chemistries available on request.
| Product Grade | Chemical Composition | Manufacturing Process | Hardness (HRC) | Application Process | Typical Application |
|---|---|---|---|---|---|
| NE-Fe-030 | C:0.3, Cr:14, Si:1.5, B:1.2, Fe:Bal | Gas Atomization | 30 | OFS/PTA/LMD | Pump impellers, sleeves, light-wear repair |
| NE-Fe-040 | C:0.4, Cr:14, Si:1.8, B:1.5, Fe:Bal | Gas Atomization | 40 | OFS/PTA/LMD | Rolls, plungers, valve seats, agricultural machinery |
| NE-Fe-050 | C:0.5, Cr:18, Si:2.0, B:2.0, Fe:Bal | Gas Atomization | 50 | OFS/PTA/LMD | Heavy-wear parts: rolls, sleeves, crusher parts, mining |
| NE-Fe-055 | C:4.5-5.5, Si:0.7-1.5, Mn:0.7-1.5, Cr:27-29, Fe:Bal | Gas Atomization | 55 | OFS/PTA/LC/AS | High-hardness surfacing for plungers, sleeves, construction & metallurgical rollers |
| NE-Fe-060 | C:5.0, Cr:28, Si:1.0, B:2.5, Mn:1.0, Fe:Bal | Gas Atomization | 60 | OFS/PTA/LMD | Severe abrasive wear: slurry pumps, extruder barrels, plow blades |
| NE-Fe-26CrNi | 26Cr, 3Ni, 1.7C, 1.6Mn, 1.6Si, 0.8Mo, Fe:Bal | VIM | 39-42 | AS/PTA/LC/FS | Good corrosion & wear, machineable stainless equivalent |
| NE-Fe-29CrB | 29Cr, 3.7B, 1.7Mn, 1.5Si, Fe:Bal | VIM | 55-60 | AS/PTA/LC/FS | Abrasion resistance, rolls, boiler tubes |
| NE-Fe-CrAl | Bal Fe, 23.5Cr, 5.3Al, 0.45Mn, 1Si | VIM | 85-90 HRB | AS/FS/LC | Boiler tubes, dimensional restoration |
How to Specify & Apply
Identify the Service Envelope
Determine the dominant wear mode (abrasion, erosion, adhesion, corrosion, oxidation), operating temperature and impact load. This narrows the grade selection to 2-3 candidates.
Match the Process
Each grade is validated for specific deposition processes. The "Application Process" field above shows HVOF, HVAF, APS, PTA, LMD, OFS or CAW compatibility.
Choose the Particle Size
Particle size controls deposit density and surface finish. Fine cuts (15-30um) for thin dense coatings; coarser cuts (45-90um) for thick build-up and high deposition rate.
Request a Sample
Most grades ship with a 1-2 kg sample for in-house process qualification. Our engineers will support parameter development on your equipment.
Other Products in Alloy Powder
Nickel-Based Alloy Powder
Ni-Cr-B-Si self-fluxing alloy powders for spray-and-fuse, PTA and laser cladding.
View →
Cobalt-Based Alloy Powder
Co-Cr-W Stellite-equivalent powders for extreme wear and high-temperature service.
View →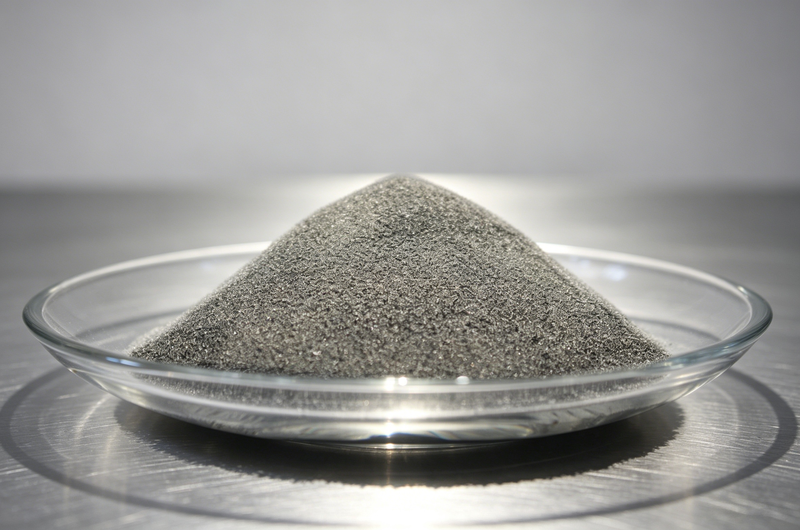
Nickel Powder Mixed with Cast Tungsten Carbide (PTA)
Ni60-based PTA hardfacing powder loaded with cast tungsten carbide for extreme abrasion.
View →